

Introduction: Why Does Every Capsule Need Accurate Weight Inspection?
In pharmaceutical manufacturing, capsule weight consistency is an important indicator of production quality. Variations in capsule filling weight may result from unstable filling processes, powder flow differences, equipment adjustments, or changes in production conditions.
Traditional sampling inspection checks only a limited number of capsules at specific intervals. Although sampling can help monitor production quality, it may not identify every individual capsule with an abnormal weight.
This is why 100% capsule weight inspection is becoming an important quality control solution for modern pharmaceutical production lines.
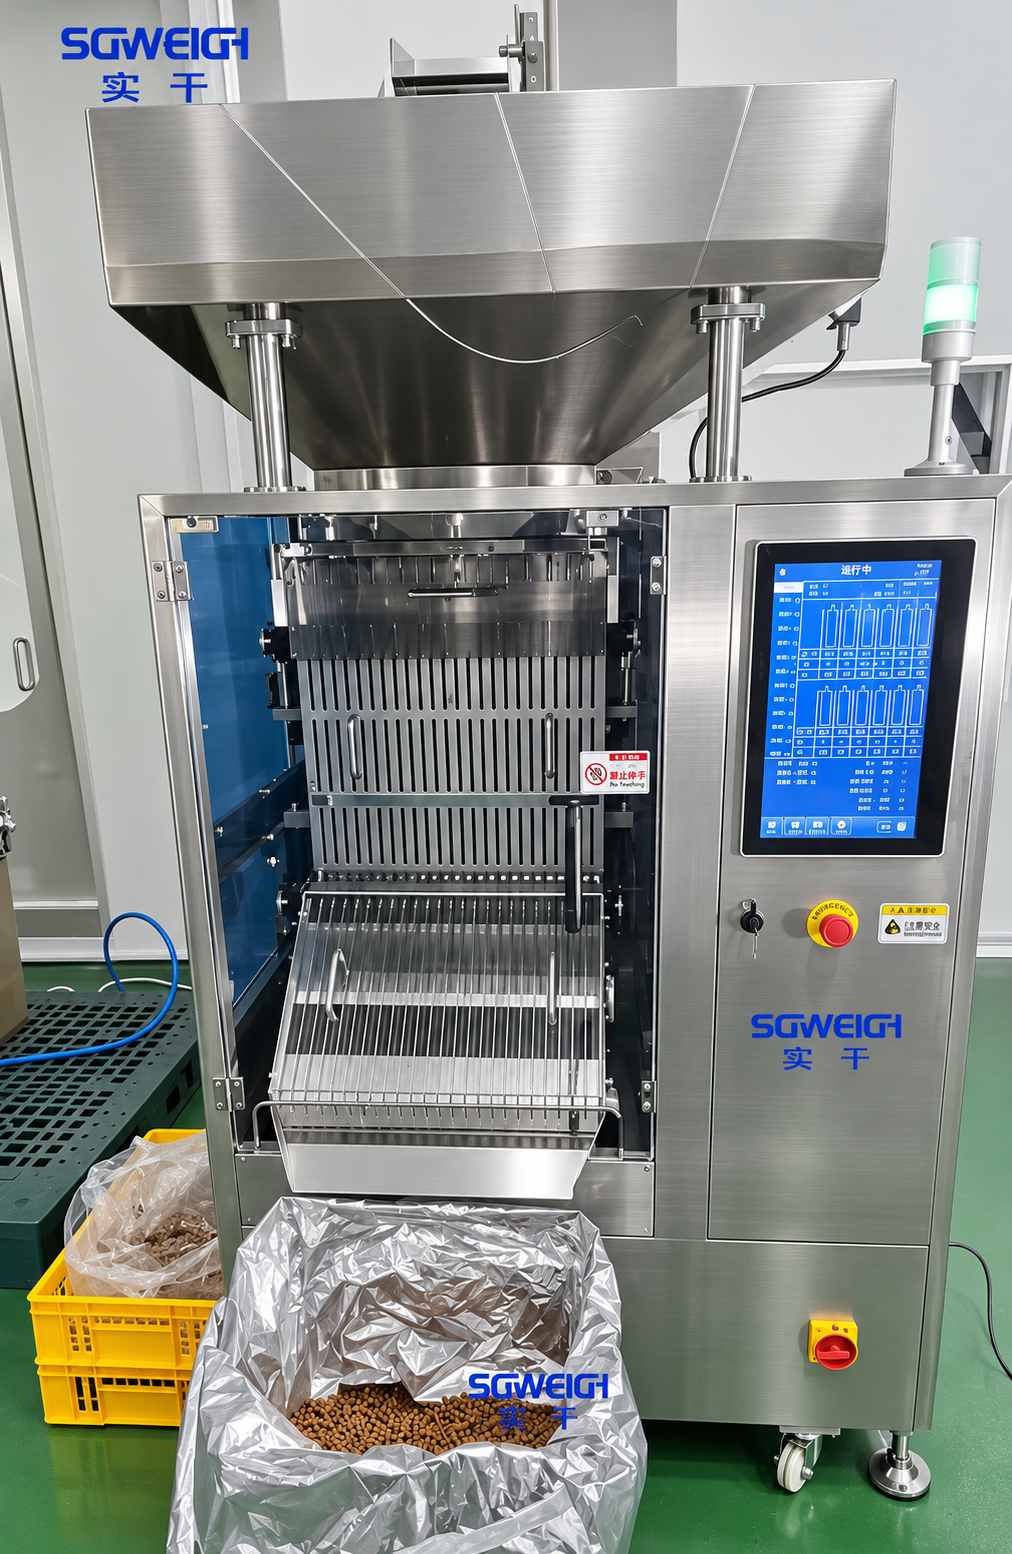
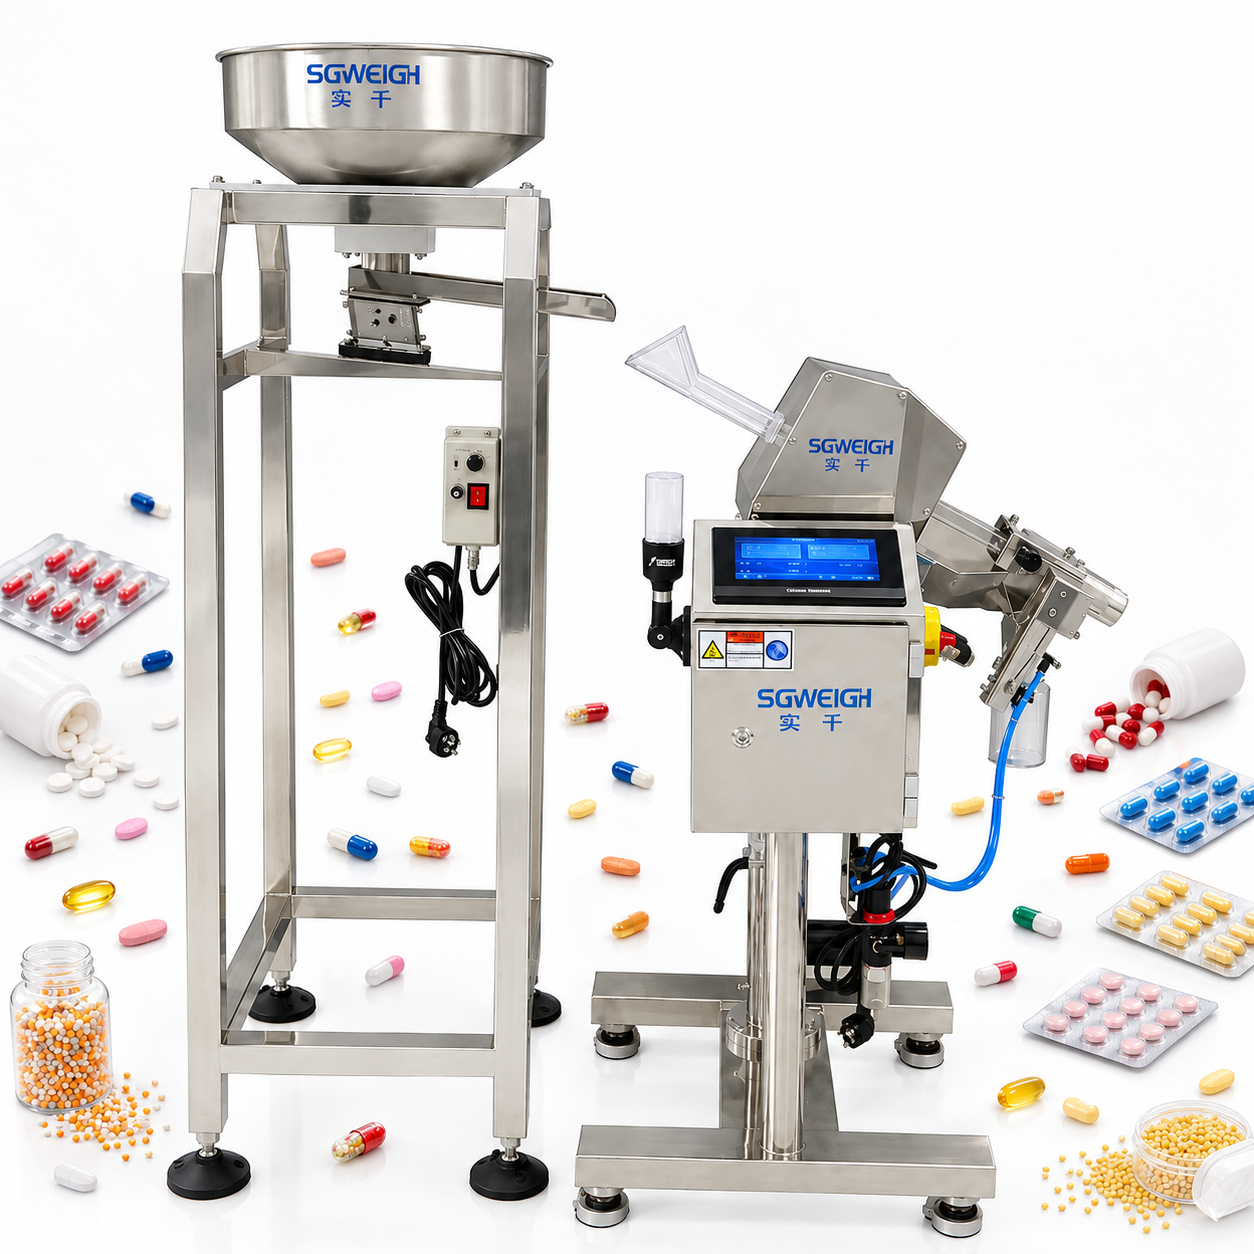
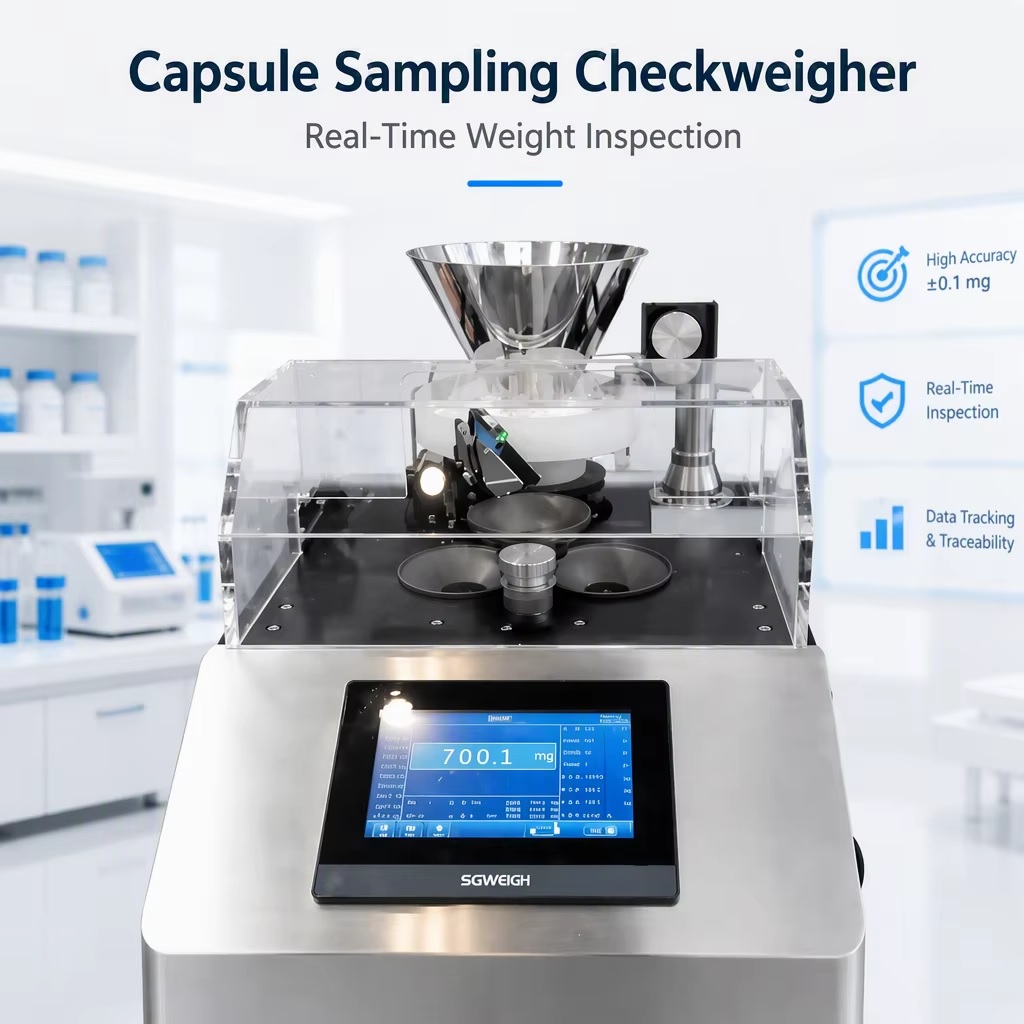
An automatic Pharmaceutical Capsule Checkweigher measures the weight of individual capsules, compares the results against preset weight limits, and automatically separates capsules that fall outside the acceptable range. By integrating an online capsule checkweigher into the production process, manufacturers can improve weight monitoring, reduce manual inspection requirements, and achieve more consistent production control.
1. What Is 100% Capsule Weight Inspection?
100% capsule weight inspection refers to the process of checking the weight of every capsule rather than inspecting only randomly selected samples.
A pharmaceutical capsule checkweigher uses a high-precision weighing sensor and an automatic feeding system to measure individual capsules during production.
The measured weight is compared with predefined upper and lower weight limits. Based on the inspection results, the system classifies capsules into qualified and rejected products.
The basic inspection process includes:
- Automatic capsule feeding and positioning.
- Individual capsule weight measurement.
- Real-time comparison with preset weight limits.
- Automatic rejection of underweight and overweight capsules.
- Collection and analysis of weighing data.
- Production statistics and quality monitoring.
This process provides manufacturers with more comprehensive weight inspection coverage and helps identify abnormal capsules before downstream packaging.
2. Why Is 100% Capsule Weight Inspection Important?
2.1 Identify Individual Capsule Weight Deviations
During capsule filling, variations in powder density, material flow, filling mechanisms, and machine operating conditions may cause weight differences between capsules.
A capsule checkweigher measures each capsule individually, helping identify products outside the specified weight range.
This is particularly important for pharmaceutical manufacturers who require consistent capsule filling quality and reliable in-process inspection.
2.2 Improve Pharmaceutical Quality Control
Weight inspection is an important part of pharmaceutical in-process quality control.
By continuously monitoring capsule weight, manufacturers can identify production deviations earlier and investigate potential problems with filling equipment or process settings.
An automatic capsule weight inspection machine provides objective measurement data that can support quality monitoring and production analysis.
It should be used as part of a broader pharmaceutical quality assurance system rather than as a replacement for other required quality tests.
2.3 Reduce Product Waste and Manual Inspection
Manual weighing and random sampling require additional labor and may not provide continuous inspection of every capsule.
An automatic capsule checkweigher can perform individual weighing and automatic sorting at production speed, reducing repetitive manual operations.
It also helps manufacturers identify process deviations earlier, potentially reducing unnecessary product waste and rework.
2.4 Support Stable High-Speed Capsule Production
Modern pharmaceutical production lines require efficient inspection solutions that can operate continuously.
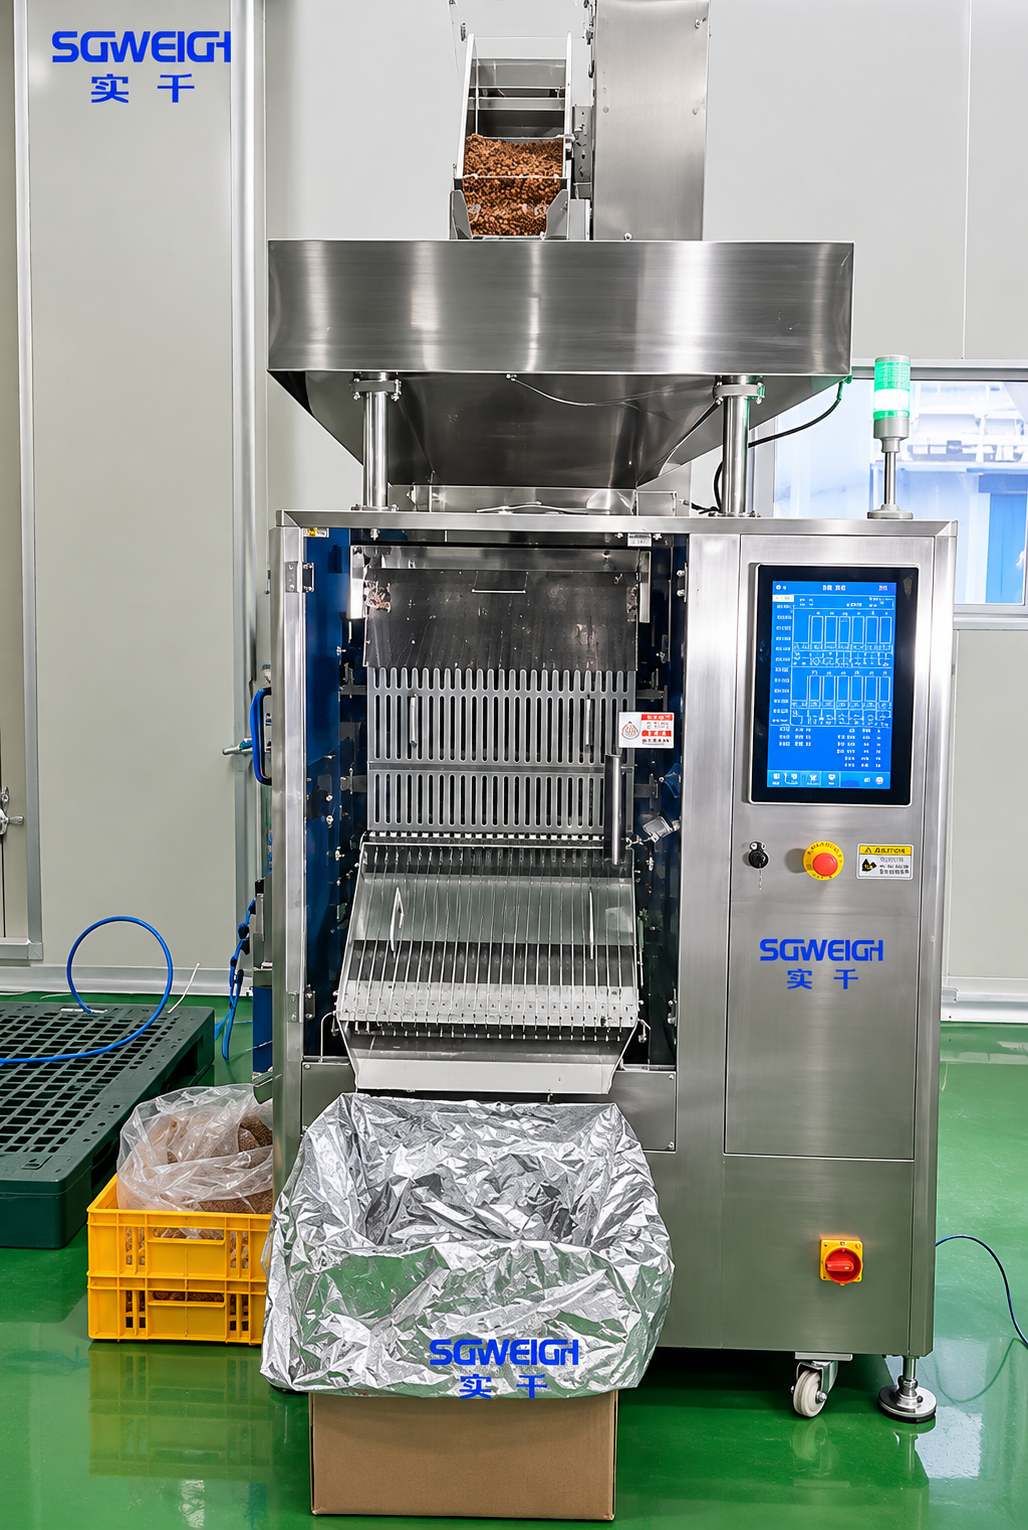
Multi-lane capsule checkweighers allow multiple capsules to be inspected through parallel weighing channels, depending on the machine configuration.
For manufacturers operating high-volume capsule production lines, a multi-channel capsule weighing system can improve inspection efficiency while maintaining individual capsule weight measurement.
2.5 Provide Traceable Production Data
Digital weighing records and production statistics help manufacturers understand weight distribution and identify trends during production.
Depending on the system configuration, a pharmaceutical capsule checkweigher can provide:
- Total inspected capsule quantity.
- Qualified and rejected capsule counts.
- Weight deviation statistics.
- Production batch information.
- Inspection reports and data export.
- User access management and audit trail functions.
For pharmaceutical applications, electronic records and audit trail functions can be configured according to applicable regulatory and validation requirements.
3. How Does an Automatic Capsule Checkweigher Work?
An automatic capsule checkweigher uses a precision weighing system to inspect capsules individually without relying entirely on manual sampling.
The typical working process consists of five stages.
Step 1: Automatic Capsule Feeding
Capsules are transferred into the feeding mechanism and arranged for stable, individual inspection.
Step 2: Individual Capsule Weighing
Each capsule is transferred to the weighing section, where a high-precision load cell measures its weight.
Step 3: Weight Comparison
The control system compares the measured weight with the preset target range, including the upper and lower weight limits.
Step 4: Automatic Sorting and Rejection
Capsules outside the specified weight range are automatically separated from qualified products through the configured rejection mechanism.
Step 5: Data Collection and Analysis
The system records inspection results and generates production statistics, helping operators monitor weight consistency and evaluate production performance.
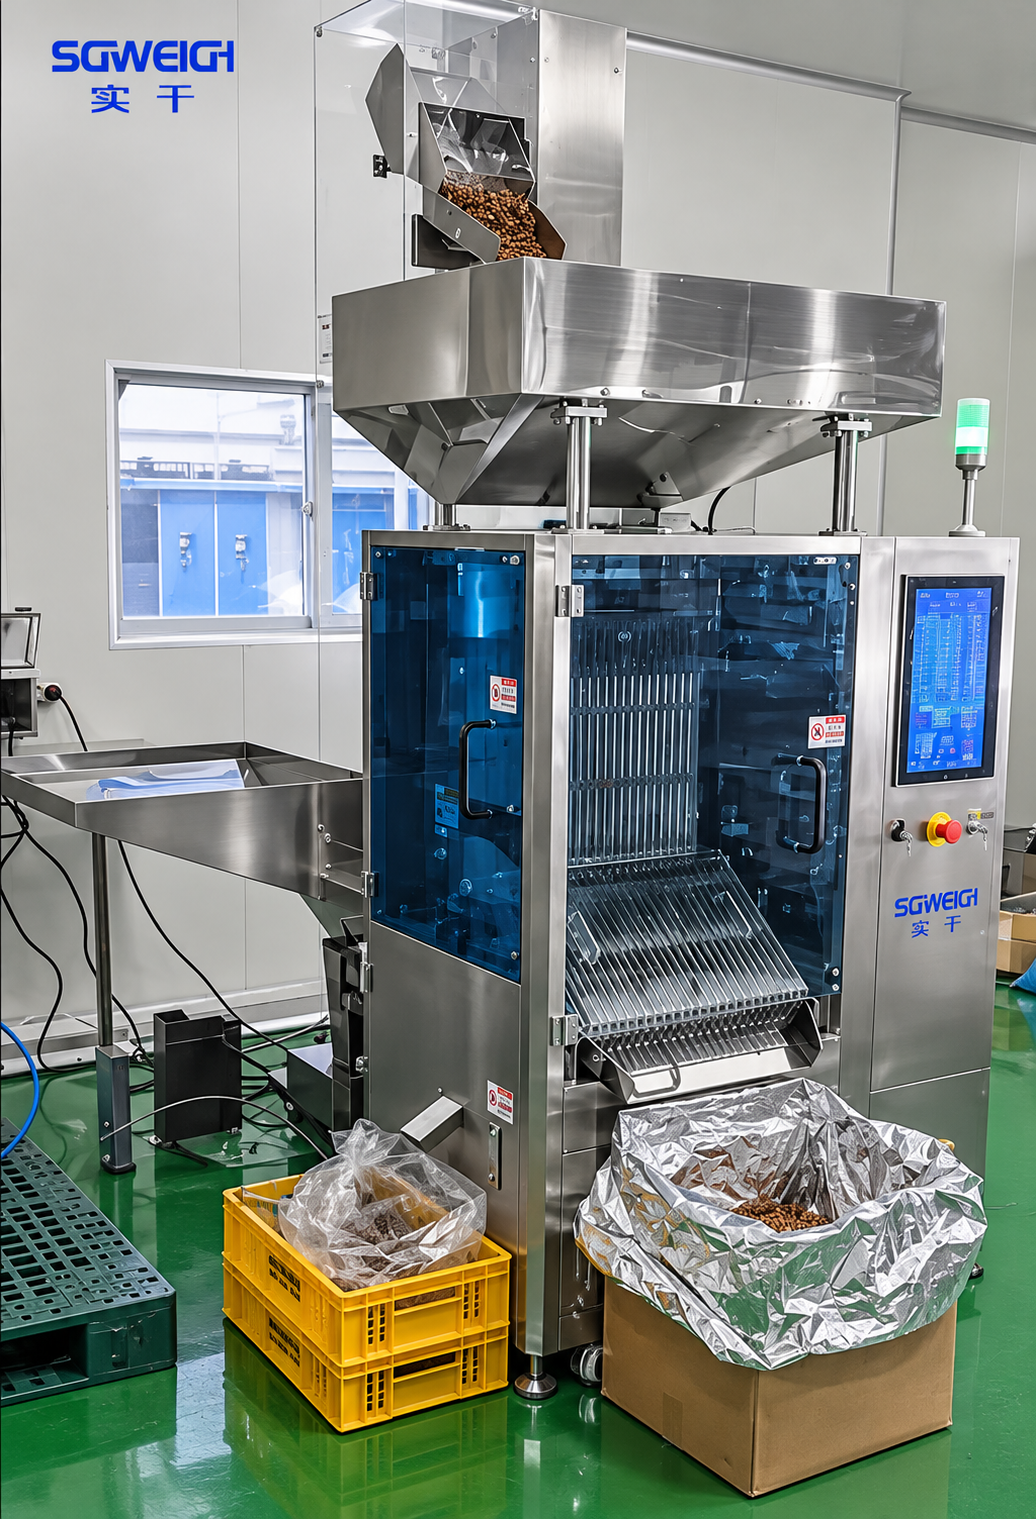
4. What Are the Advantages of a High-Precision Pharmaceutical Capsule Checkweigher?
A high-precision capsule checkweigher is designed for applications requiring individual capsule weight measurement and reliable automatic inspection.
Key features may include:
- High-Precision Weighing Sensor: Measures individual capsule weight with a suitable weighing resolution and repeatability.
- Individual Capsule Inspection: Checks capsules one by one instead of relying only on random sampling.
- Automatic Rejection System: Separates capsules outside preset weight limits.
- Multi-Lane Inspection: Supports parallel capsule weighing to improve production efficiency.
- User-Friendly Touchscreen: Allows operators to configure weighing parameters and monitor production results.
- Production Data Statistics: Displays inspection quantities, qualified products, rejected products, and weight information.
- Easy Cleaning and Maintenance: A suitable hygienic design helps facilitate cleaning and routine maintenance.
- Production Line Integration: Can be configured to connect with upstream capsule filling equipment and downstream collection systems.
Actual weighing accuracy, inspection speed, capsule size compatibility, and channel quantity depend on the machine model and production conditions.
5. Applications of Capsule Checkweighers in Pharmaceutical Manufacturing
Automatic capsule checkweighers can be used in different pharmaceutical production environments, including:
- Hard gelatin capsule production.
- HPMC vegetarian capsule manufacturing.
- Powder-filled capsule inspection.
- Pharmaceutical capsule filling lines.
- Nutraceutical and dietary supplement capsule production.
- Individual capsule weight inspection before packaging.
The equipment can be configured according to capsule dimensions, product characteristics, production speed, and inspection requirements.
It is important to note that capsule weight inspection verifies product weight within specified limits. It does not independently confirm active pharmaceutical ingredient content, drug potency, or uniformity of dosage units. Those characteristics require appropriate validated analytical testing.
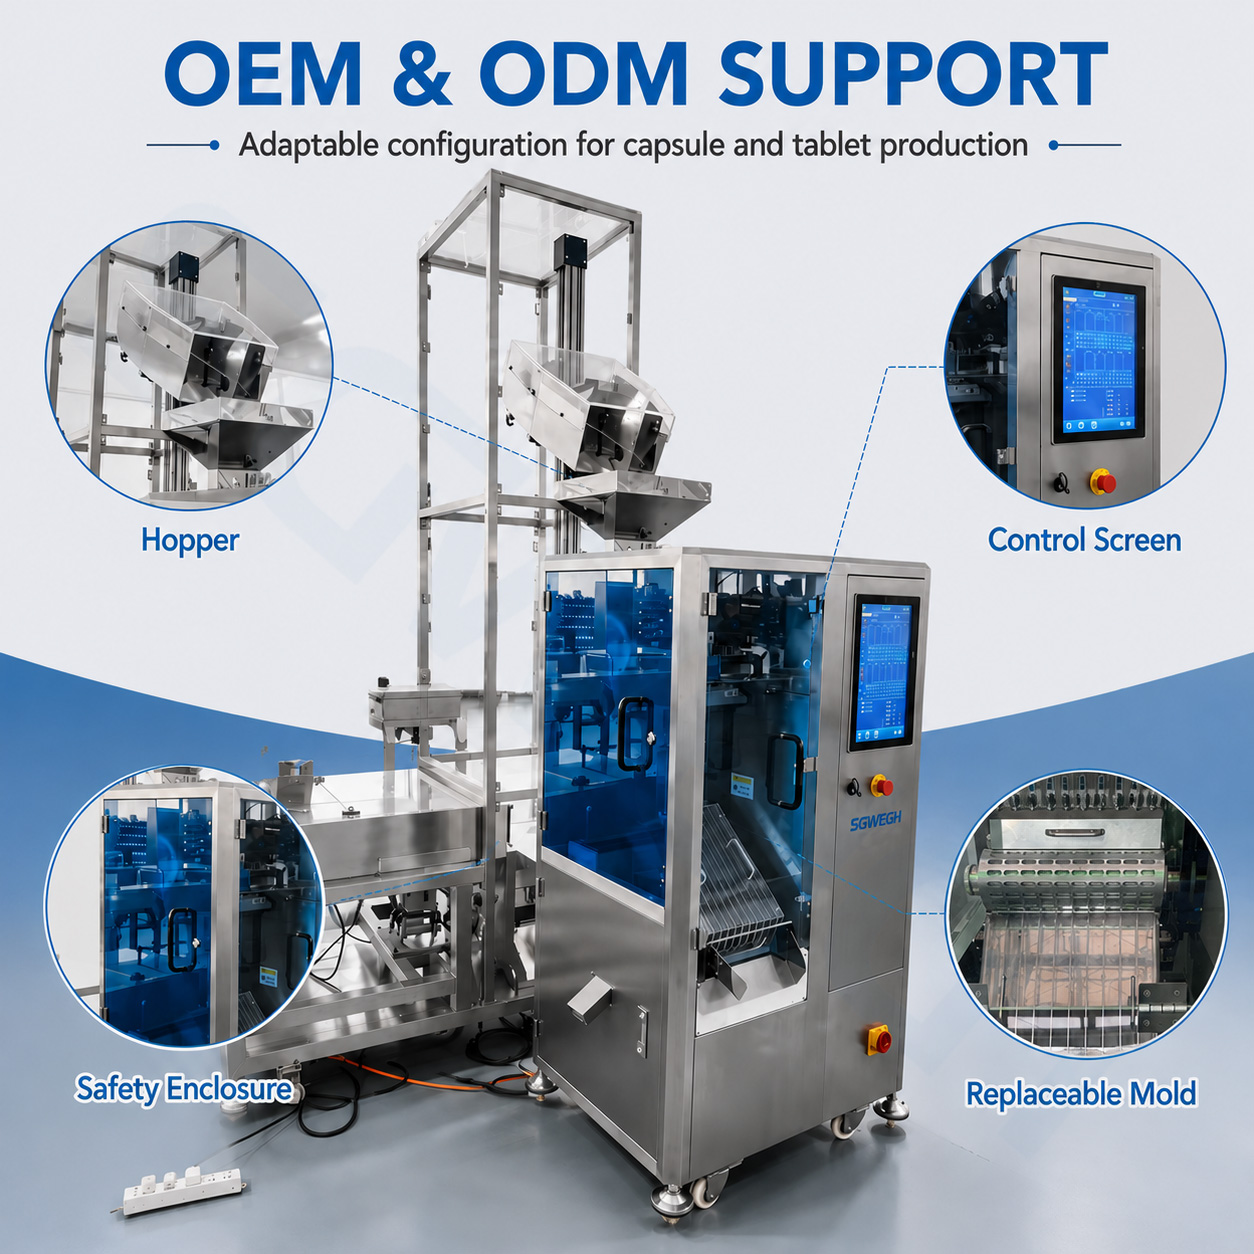
6. Why Choose SGWEIGH Capsule Checkweigher Solutions?
SGWEIGH focuses on industrial weighing and inspection equipment, providing capsule checkweigher solutions for pharmaceutical and related manufacturing applications.
Our capsule weighing systems can be configured according to different production requirements, including individual capsule weighing, multi-lane inspection, automatic weight sorting, and production data management.
Whether you need a compact capsule checkweigher for precision inspection or a multi-lane system for high-capacity production, SGWEIGH can help evaluate the appropriate equipment configuration.
Contact SGWEIGH to discuss your capsule inspection requirements and receive a customized capsule checkweigher solution.
TAGS